For vegetable processing plant managers and production engineers, the washing stage is a critical control point. It’s not just about cleaning produce; it’s about maintaining throughput, meeting food safety standards, and keeping operational costs under control. Yet, many facilities struggle with three persistent, interconnected challenges that directly impact profitability and compliance.
The first is inefficient drainage. If water pools on the belt or carries soil back onto freshly cleaned produce, you are wasting water, energy, and compromising final product quality. The second is contamination risk from belt degradation. Standard mesh belts fray at the edges over time. Those tiny, loose fibers can shed directly into your food stream, creating a serious safety hazard and potential recall trigger. The third is downtime from misalignment. In wet, high-moisture environments, belts are prone to wandering off track, leading to edge damage and unplanned stoppages.
Annilte’s Polyester Mesh Conveyor Belts are engineered specifically to eliminate these pain points.
Why Annilte’s Polyester Mesh Belt is the Preferred Choice for Vegetable Cleaning
We understand that your conveyor belt is not just a transport medium; it is a critical piece of your hygiene and efficiency system. Our polyester mesh belts are built on a foundation of high-tenacity, food-grade PET material, combined with manufacturing processes designed for the realities of a wet processing environment.
Unmatched Drainage and Cleaning Efficiency
The open-mesh structure of our polyester belts allows water, steam, and cleaning agents to pass through freely. This immediate drainage prevents cross-contamination from dirty wash water and accelerates the drying process, whether you are using air knives or a drying tunnel. Unlike solid belts, there are no hidden crevices for bacteria or vegetable debris to accumulate, making sanitation faster and more effective.
Reinforced Edge Technology: Solving the Fiber Shedding Problem
This is a critical differentiator. Plain woven belts are vulnerable at the edges where they are cut. Over time, mechanical friction against the machine frame causes the yarns to fray and shed fibers into the product stream.
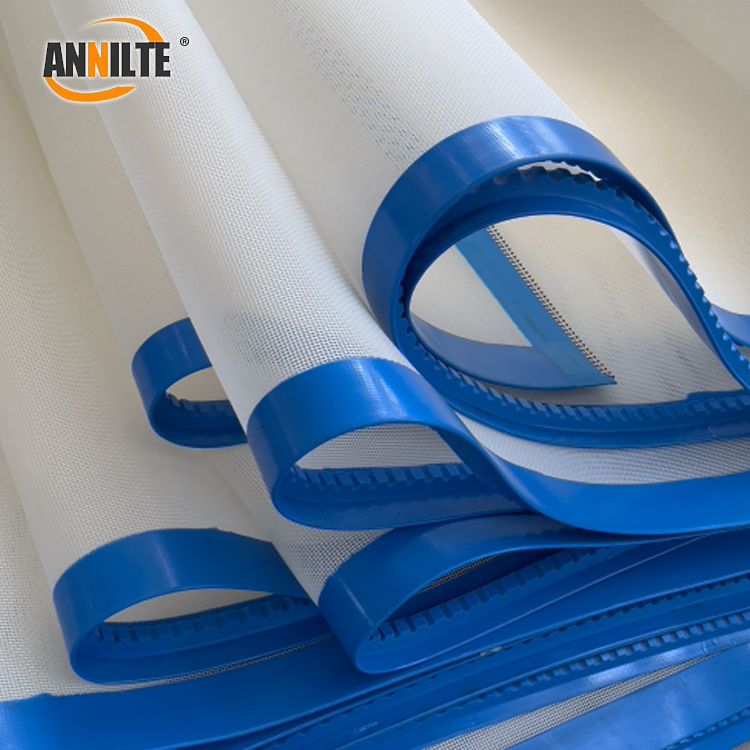
Annilte addresses this with proprietary high-frequency edge reinforcement. We fully encapsulate the mesh edges with food-grade PU or PVC. This creates a durable, hygienic barrier that seals in all fibers. The result is zero contamination risk from belt shedding, improved lateral stability, and a significantly longer service life for the belt.
Stable Tracking in Wet Environments
Misalignment is a primary cause of belt failure and costly downtime. Our polyester mesh belts can be equipped with precision V-guides or tracking bars on the underside. These guides interface directly with your machine’s grooves, ensuring the belt stays perfectly centered, even under the heavy moisture loads typical of vegetable washing lines. This protects the belt edges from wear and prevents spillage.
Comprehensive Food Safety Compliance
Trust is built on verification. Annilte’s food-grade polyester mesh belts are manufactured using 100% virgin PET polymers and comply with FDA (US Food and Drug Administration) and EU 1935/2004/EC standards for direct food contact. This gives you the documentation and confidence you need for your HACCP and ISO 22000 programs.
Customization for Your Specific Production Layout
No two vegetable processing lines are identical. Annilte provides tailored belting solutions to match your exact requirements:
- Inclined Conveying: We heat-weld food-grade baffles (cleats) directly onto the mesh surface. This creates enclosed pockets that prevent washed vegetables from rolling back during steep elevations.
- Side Containment: For loose leafy greens or diced vegetables, we can attach corrugated sidewalls (skirts) to keep product on the belt.
- Custom Mesh Openings: Choose from a range of mesh sizes to optimize drainage and airflow for your specific product—whether you are processing delicate herbs or root vegetables.
- Belt Types: Available in endless spliced belts or with mechanical fasteners for easy installation.

R&D Team
Annilte has a research and development team consisting of 35 technicians. With strong technical research and development capabilities, we have provided conveyor belt customization services for 1780 industry segments, and gained recognition and affirmation from 20,000+ customers. With mature R&D and customization experience, we can meet the customization needs of different scenarios in various industries.

Production Strength
Annilte has 16 fully automated production lines imported from Germany in its integrated workshop, and 2 additional emergency backup production lines. The company ensures that the safety stock of all kinds of raw materials is not less than 400,000 square meters, and once the customer submits an emergency order, we will ship the product within 24 hours to respond to the customer's needs efficiently.
As a leading Chinese conveyor belt manufacturer with 17 years of industry experience, Annilte is proud to hold both ISO quality management certification and the RoHS environmental directive. Our manufacturing facilities meet “Green Factory” standards, and we are also an internationally recognized SGS Gold Supplier.
We offer a comprehensive range of customizable belt solutions under our own brand "ANNILTE", designed to meet diverse industrial needs.
Should you require further information about our products or capabilities, please do not hesitate to contact us.
WhatsApp: +86 185 6019 6101 Tel/WeChat: +86 185 6010 2292
E-mail: 391886440@qq.com Website: https://www.annilte.net/
Post time: Sep-28-2026