Metal Mesh Is Costing You More Than You Think. Here’s What Food Plant Engineers Are Switching To.
If you manage a vegetable processing line, you already know the drill: wash, drain, dry, cool. The belt running through that sequence is the silent workhorse nobody talks about—until it fails an audit, contaminates a batch, or grinds production to a halt.
For decades, stainless steel mesh was the default. It was strong, it was metal, it felt “industrial.” But engineering managers across Europe and North America are quietly reevaluating that assumption. The reason isn’t a single dramatic failure. It’s the accumulation of small, expensive realities that metal mesh brings to a food-grade environment.
The Three Quiet Problems with Metal Mesh
Problem One: The Fragment Risk Nobody Wants to Document. Metal mesh belts wear. Edges fray, welds fatigue, and tiny stainless fragments can migrate into the product stream. One recall—even a precautionary one—costs far more than a decade of belt replacements. Your QA team knows this. Your auditors know this. The question is whether your belt specification reflects it.
Problem Two: Cleaning Is Never Actually “Clean.” Metal mesh has a deceptive open structure. Product lodges in the interstices between wires. High-pressure washdown pushes material deeper rather than flushing it out. Over time, bacterial harborage points develop in places your sanitation team cannot visually inspect. For ready-to-eat vegetable lines, this is a compliance exposure that compounds with every production shift.
Problem Three: The Energy Bill You Can’t See. In drying and cooling applications, airflow is everything. Metal mesh creates turbulent resistance. Air that should pass through the product bed gets deflected, and your burner works harder to compensate. At scale, that inefficiency is a line item your CFO notices.
Why Polyester Mesh Changes the Equation
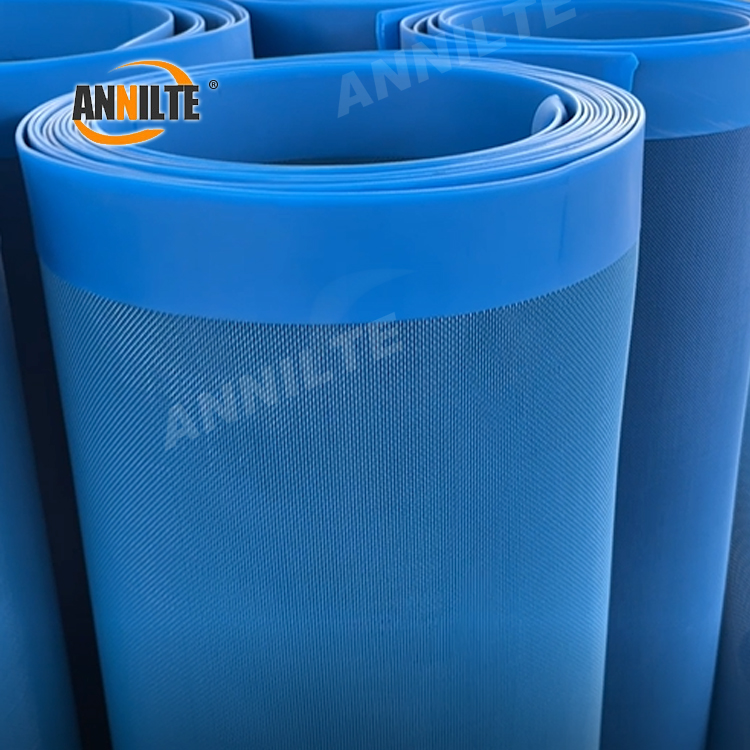
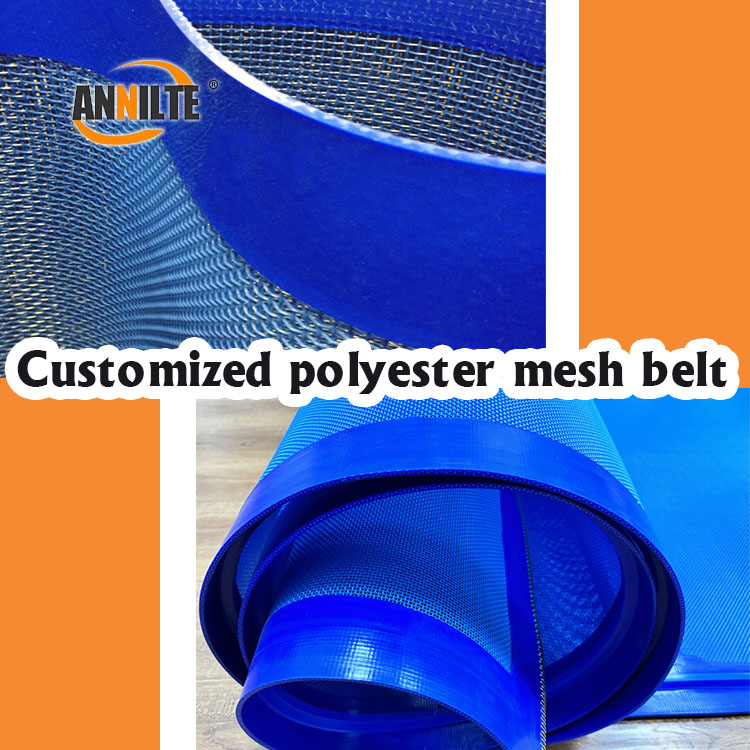
Annilte manufactures polyester mesh conveyor belts specifically for the realities of food processing. Not as a “metal alternative,” but as an engineered solution that addresses each of the failure modes above.
Zero Metal Contamination Risk. The belt is 100% polyester monofilament. There is no metal to fragment, no weld to fatigue, no edge to shed. For plants running metal detectors downstream, the belt simply disappears from your foreign-body risk assessment. That’s one less variable to monitor, one less audit finding to defend.
Open Area You Can Actually Clean. Polyester mesh delivers open area percentages that metal simply cannot match at equivalent strength. Annilte’s standard 2-shed and 3-shed weaves achieve air permeability exceeding 20,000 m³/m²h on select specifications. Water passes through instantly. Product doesn’t lodge because there are no inter-wire crevices to trap it. High-pressure washdown flushes clean in a single pass.
Chemical Resistance That Survives Your Sanitation Program. Polyester resists the acids, alkalis, and cleaning agents that food plants use daily. It maintains dimensional stability across a temperature range from -40°C to +150°C. Your sanitation team can use the chemistry they need without worrying about belt degradation—or the documentation that follows a belt failure during a production run.
Energy Efficiency That Shows Up on the P&L. Higher air permeability means less resistance. Your dryer or cooler moves the same volume of air with less fan horsepower, or moves more air at the same horsepower. Either way, the belt pays for itself in operating cost, not just purchase price.
What Separates Annilte from the Trading Companies
Most suppliers selling “polyester mesh belts” are resellers. They source from weaving mills, warehouse inventory, and ship when an order comes in. That model works for commodity purchases. It fails when your line is down and you need a belt with a specific mesh opening, a custom width, and an edge finish that matches your conveyor frame.
Annilte is a manufacturer. We operate 16 fully automated production lines in our integrated workshop, with an additional 2 emergency backup lines reserved specifically for urgent orders. Our raw material safety stock exceeds 400,000 square meters. When a customer with a stopped line submits an emergency order, we ship within 24 hours.
Our engineering team includes 35 full-time R&D technicians who have delivered custom conveyor solutions across 1,780 industry segments. That experience matters when your application isn’t standard—when the mesh size needs adjustment, when the edge needs reinforcement, when the joint needs to run through a specific pulley diameter without tracking issues.
We serve 20,000+ customers globally, including 18 Fortune 500 companies. Our facilities hold ISO certification and SGS Gold Supplier status. The belts are manufactured to FDA and EU food contact standards, with documentation your auditors will accept.
The Specification Conversation You Should Be Having
If you are still running metal mesh in a vegetable washing or drying line, the question isn’t whether polyester is “good enough.” The question is how much the metal risk, the cleaning burden, and the energy waste are costing you per year.
Send us your line specifications—belt width, mesh opening requirements, temperature range, and chemical exposure. Our engineers will respond with a specific recommendation, not a generic catalog page. For urgent replacement needs, include your downtime window and we will confirm shipping feasibility within 24 hours.

R&D Team
Annilte has a research and development team consisting of 35 technicians. With strong technical research and development capabilities, we have provided conveyor belt customization services for 1780 industry segments, and gained recognition and affirmation from 20,000+ customers. With mature R&D and customization experience, we can meet the customization needs of different scenarios in various industries.

Production Strength
Annilte has 16 fully automated production lines imported from Germany in its integrated workshop, and 2 additional emergency backup production lines. The company ensures that the safety stock of all kinds of raw materials is not less than 400,000 square meters, and once the customer submits an emergency order, we will ship the product within 24 hours to respond to the customer's needs efficiently.
As a leading Chinese conveyor belt manufacturer with 17 years of industry experience, Annilte is proud to hold both ISO quality management certification and the RoHS environmental directive. Our manufacturing facilities meet “Green Factory” standards, and we are also an internationally recognized SGS Gold Supplier.
We offer a comprehensive range of customizable belt solutions under our own brand "ANNILTE", designed to meet diverse industrial needs.
Should you require further information about our products or capabilities, please do not hesitate to contact us.
WhatsApp: +86 185 6019 6101 Tel/WeChat: +86 185 6010 2292
E-mail: 391886440@qq.com Website: https://www.annilte.net/
Post time: Oct-19-2026