What Buyers Searching "Magnetic Separator Conveyor Belt" Are Really Looking For
People typing this phrase into Google are rarely browsing. They are most likely standing next to a magnetic separator that is down for repair, or locking in a belt supplier for a new machine order. Behind this search term sit three distinct buyer types: end users who need a replacement part, separator manufacturers sourcing a component supplier, and industrial distributors looking to expand their product line. What all three share is this—they already know a general-purpose conveyor belt won't solve the problem. They are looking for a belt built to the operating conditions of magnetic separation equipment.
Annilte's customization experience in this specific niche maps directly onto the core concerns of all three buyer types.
Three "Incompatible" Requirements Magnetic Separators Place on Conveyor Belts
A standard conveyor belt is designed to carry bulk material smoothly. A belt on a magnetic separator has a different job: fling ferrous contamination out of a magnetic field. These two tasks demand almost opposite things from a belt.
First, the belt must absorb impact, not carry load. Captured ferrous items "fly" out of the material stream and strike the belt surface with kinetic energy. Scrap fragments, stamped offcuts, and casting burrs are all potential puncture sources. The rubber cover on an ordinary belt develops tears within weeks, then moisture enters the fabric layers, delamination follows, and the belt fails. Annilte's approach is to match cover compound thickness and tear-resistant fabric construction to the sharpness of the material being separated—adding a stainless steel armored layer where necessary. This is not a checkbox on a standard product sheet; it is a parameter in the customization process.
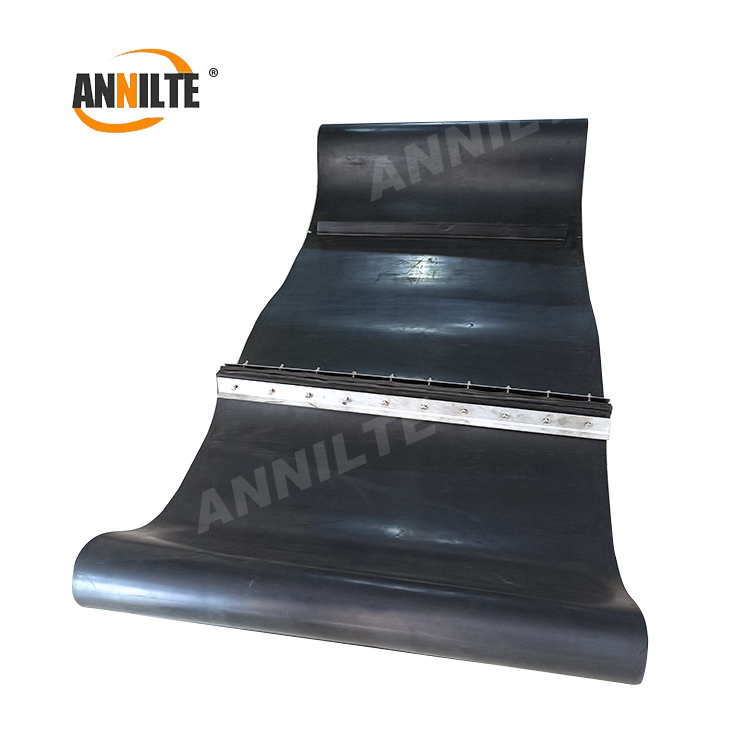
Second, cleats must be "grown" into the belt, not attached to it. Discharge depends on transverse cleats pushing ferrous items out of the magnetic zone. Bonded or bolted cleats eventually peel off under repeated impact—and once a cleat is gone, ferrous items slide back and forth across the belt, accelerating wear exponentially. Annilte uses vulcanized, integrally molded cleats: cleat and belt body are cured as one rubber unit, with no interface to delaminate. Cleat height and spacing are customized to the customer's magnetic zone length and pulley dimensions, rather than forced into a fixed catalog size.
Third, the splice is where failure starts—so eliminate the splice. A field-spliced belt always breaks first at the joint. The ideal form for separator belts is a factory-made endless belt, with circumference accurate to the millimeter and ready to install. Annilte's endless belt customization covers the full parameter set—width, circumference, cleat spacing. Customers simply provide the pulley center distance to place an order.
Specify by Operating Condition, Not by Stock List
Many suppliers quote only a few standard sizes, forcing buyers to compromise between "too thin to last" and "too thick to fit." Annilte's customization logic works backward from the operating condition:
| What the customer describes | Recommended belt configuration |
|---|---|
| Sharp ferrous items, frequent puncture | Thicker cover + high tear-resistant fabric + optional stainless steel armor |
| High material temperature (sinter, clinker) | Heat-resistant rubber compound to prevent cover hardening and cracking |
| Oily environment (common in scrap recycling) | Oil-resistant cover to prevent rubber swelling |
| Tight equipment space, cleat interference | Cleat height and spacing customized to measured dimensions |
| Extremely high cost of belt-change downtime | Seamless endless belt + fast replication of historical specs |
The value of this method: buyers don't need to become belt experts. They only need to explain what their separator is separating and where the belt is failing; Annilte's technical team handles the parameter mapping. Sixteen years of customization R&D, a 35-person engineering team, and service across 1,780 industry segments feed into the accuracy of that mapping. The cost of specifying the wrong belt once far exceeds the price difference of customizing it correctly.
Three Buyer Types, Three Decision Paths
End users (replacement sourcing): Their concerns are "how fast can I get it, will it fit, how long will it last." For customers who have previously supplied equipment parameters, Annilte can rapidly replicate from historical specs, with emergency orders shipping within 24 hours. Raw material safety stock is maintained at no less than 400,000 square meters, and routine custom orders are scheduled quickly after spec confirmation.
Separator manufacturers (OEM supply): Their concerns are locked specifications, batch consistency, and delivery synchronized with machine orders. The belt is a sub-component of the whole machine—any batch deviation surfaces as an end-customer complaint. Annilte's ISO quality system, SGS certification, and supply chain experience serving 18 Fortune 500 companies form the basis for entering an OEM tier-two supplier program.
Industrial distributors: Their concern is "selling custom belts without building an in-house technical team." The distributor provides the end customer's equipment model and operating condition description; Annilte completes specification and production; the distributor delivers under its own brand and earns a technical-service premium rather than a simple markup.

R&D Team
Annilte has a research and development team consisting of 35 technicians. With strong technical research and development capabilities, we have provided conveyor belt customization services for 1780 industry segments, and gained recognition and affirmation from 20,000+ customers. With mature R&D and customization experience, we can meet the customization needs of different scenarios in various industries.

Production Strength
Annilte has 16 fully automated production lines imported from Germany in its integrated workshop, and 2 additional emergency backup production lines. The company ensures that the safety stock of all kinds of raw materials is not less than 400,000 square meters, and once the customer submits an emergency order, we will ship the product within 24 hours to respond to the customer's needs efficiently.
As a leading Chinese conveyor belt manufacturer with 17 years of industry experience, Annilte is proud to hold both ISO quality management certification and the RoHS environmental directive. Our manufacturing facilities meet “Green Factory” standards, and we are also an internationally recognized SGS Gold Supplier.
We offer a comprehensive range of customizable belt solutions under our own brand "ANNILTE", designed to meet diverse industrial needs.
Should you require further information about our products or capabilities, please do not hesitate to contact us.
WhatsApp: +86 185 6019 6101 Tel/WeChat: +86 185 6010 2292
E-mail: 391886440@qq.com Website: https://www.annilte.net/
Post time: Nov-13-2026