When a gypsum board production line belt fails, the post-mortem usually points to the belt: surface wear, edge cracking, splice separation, tracking drift. But in most cases, the belt is not the root cause. It is the component that absorbed a mismatch created upstream—by line speed ratios, tensioner capacity, or section-to-section handoff design.
The previous guide addressed belt selection by line position. This guide takes a different angle: how to specify the belt as an integrated component of your production line’s architecture. If you are an equipment OEM, a line integrator, or a plant engineer replacing belts across multiple sections, this is the framework that prevents repeat failures.
Line Speed Ratios and Why They Kill Belts
1.1 The Speed Mismatch Problem
A gypsum board line does not run at one speed. The forming section, hydration conveyor, and drying section often operate at different speeds to manage board spacing and curing time. Patent literature on wallboard line control systems describes exactly this: the hydration section conveyor and drying section conveyor are set at different speeds, with a control module calculating gap adjustments between boards based on the speed difference.
What this means for belt selection:
If your forming belt and the downstream transfer belt run at different surface speeds, the board experiences a shear force at the handoff point. The belt with the softer cover or the less stable tension absorbs that shear as surface wear and edge stress. Over time, the belt that “looks fine on paper” becomes the one that fails first.
Action: Map the surface speed of every belt in your line. Any handoff where speed differs by more than 2–3% needs a belt specification that accounts for slip and shear, not just tensile strength.
1.2 Acceleration Zones
Some line designs accelerate the board after cutting to create gap for the drying section. The belt in the acceleration zone sees rapid tension changes that a steady-state tensile rating does not capture. A belt with a vulcanized joint rated at 85% of body strength may still fail if the acceleration profile exceeds the joint’s fatigue tolerance.
Ask your belt supplier: What is the dynamic tension tolerance of this belt under repeated acceleration cycles, not just the static tensile strength?
Tensioner Capacity Is a Hard Constraint, Not a Suggestion
2.1 The Small Tensioner Trap
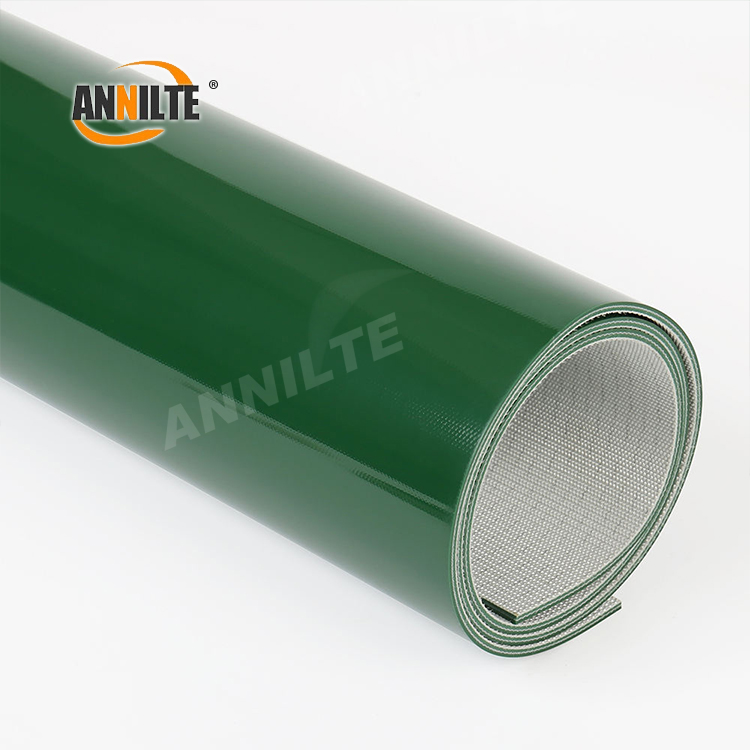
Many gypsum board lines, especially older or compact designs, have tensioners with limited stroke and force capacity. A real-world retrofit case from a large plasterboard plant in Jiaxing illustrates the problem: the customer’s equipment had small tensioners, and standard belt options either could not achieve proper tension or required excessive take-up that shortened splice life. The solution was a specially selected polyester-rubber power belt with tension characteristics matched to the small tensioner’s capability.
The lesson: A belt’s modulus (its resistance to stretching under load) must match your tensioner’s ability to stretch it. A high-modulus belt on a small tensioner will either slip (if under-tensioned) or overload the tensioner bearings (if over-tensioned).
2.2 How to Specify Tension Compatibility
| Your Tensioner Situation | Belt Characteristic Needed |
|---|---|
| Short stroke, limited force | Lower modulus, higher elongation at working tension |
| Long stroke, high force | Standard or high modulus, low elongation |
| Unknown or variable | Request tension-elongation curve from supplier |
Do not accept a belt datasheet that lists only “tensile strength.” Ask for the elongation at 1% tension and compare it to your tensioner’s available stroke.
Section Handoffs: Where Tracking Failures Are Born
3.1 The Handoff Alignment Window
A belt that tracks perfectly on its own frame can still cause the board to misalign at the next section if the two belts are not coplanar and parallel within a tight tolerance. The board does not know the belt is tracking well—it only knows that the gap between sections is uneven.
Typical failure pattern:
- Forming belt tracks true.
- Transfer belt tracks true.
- Board drifts at the handoff because the transfer belt’s centerline is 2 mm off from the forming belt’s centerline.
- Edge damage appears on one side of the board.
- Operator adjusts belt tracking to compensate, introducing actual misalignment on the transfer belt.
3.2 Belt Characteristics That Reduce Handoff Sensitivity
- Consistent width tolerance: If the belt width varies by more than ±1 mm across its length, the effective centerline shifts as the belt runs.
- Square, low-profile joints: A thick joint lifts the board momentarily at the splice, which can cause a micro-shift at the handoff.
- Symmetric edge construction: Belts with asymmetric edge reinforcement pull to one side under tension.
The Line-Integration Checklist
Use this when specifying belts for a new line or a multi-section replacement. It goes beyond the single-belt checklist in the previous guide.
| Line-Level Factor | What to Document | Why It Matters for Belt Selection |
|---|---|---|
| Speed ratio between sections | % speed difference at each handoff | Determines shear and slip requirements |
| Acceleration/deceleration profile | Ramp time, frequency per shift | Affects splice fatigue life |
| Tensioner type and stroke | Available take-up, force capacity | Constrains belt modulus selection |
| Section centerline alignment tolerance | mm deviation between adjacent belt centerlines | Sets belt width and tracking sensitivity |
| Board gap control method | Sensor type, adjustment range | Affects belt speed stability requirements |
| Emergency stop frequency | Stops per day, deceleration rate | Stress on joints and covers |
| Ambient conditions per section | Temp, humidity, dust load | Cover compound and splice method |
Why “Line-Matched” Belts Cost Less Over Three Years
A belt priced 15% lower per meter but failing 40% sooner is not cheaper. The calculation is straightforward:
Cost per year = (Belt price ÷ Service life in years) + (Downtime cost per hour × Hours per replacement) + (Labor cost per replacement)
For a forming line belt that fails six months early, the downtime alone—even at a conservative four-hour replacement—can exceed the entire price difference between a commodity belt and a line-matched belt.
Annilte’s approach with line integrators and multi-section buyers is to review the line layout and speed profile before recommending belt specifications. The company’s production capability includes dedicated forming belt lines and a raw material safety stock above 400,000 m², but the specification process starts with the line, not the catalog.

R&D Team
Annilte has a research and development team consisting of 35 technicians. With strong technical research and development capabilities, we have provided conveyor belt customization services for 1780 industry segments, and gained recognition and affirmation from 20,000+ customers. With mature R&D and customization experience, we can meet the customization needs of different scenarios in various industries.

Production Strength
Annilte has 16 fully automated production lines imported from Germany in its integrated workshop, and 2 additional emergency backup production lines. The company ensures that the safety stock of all kinds of raw materials is not less than 400,000 square meters, and once the customer submits an emergency order, we will ship the product within 24 hours to respond to the customer's needs efficiently.
As a leading Chinese conveyor belt manufacturer with 17 years of industry experience, Annilte is proud to hold both ISO quality management certification and the RoHS environmental directive. Our manufacturing facilities meet “Green Factory” standards, and we are also an internationally recognized SGS Gold Supplier.
We offer a comprehensive range of customizable belt solutions under our own brand "ANNILTE", designed to meet diverse industrial needs.
Should you require further information about our products or capabilities, please do not hesitate to contact us.
WhatsApp: +86 185 6019 6101 Tel/WeChat: +86 185 6010 2292
E-mail: 391886440@qq.com Website: https://www.annilte.net/
Post time: Oct-29-2026