Chocolate cooling tunnels are where good belts go to fail. Not because the belt is low quality in general terms, but because the conditions inside a tunnel expose three specific weaknesses that standard food-grade PU specifications don‘t address: release behavior as the chocolate contracts, residue buildup that hardens into places brushes can’t reach, and splice geometry that changes once the belt goes cold.
This is written for distributors specifying belts for confectionery customers, and for plant buyers who are tired of swapping belts before their time.
Why Standard PU Isn‘t Automatically the Right PU
Most food-grade PU belts will pass the compliance check. FDA, EU 10/2011—those are table stakes. What they won’t tell you is how the top surface behaves when warm chocolate is poured onto it and then cooled to tunnel temperature.
Esbelt‘s documentation for chocolate cooling applications is unusually specific on this point: they call out low adhesion of the top coating as a requirement for facilitating product transfer and positioning, and note that the surface should be “brilliant, smooth, homogeneous, non-porous” to prevent chocolate accumulation at the base of the product . That’s a different conversation than generic “food grade.” It’s about whether the surface chemistry actually releases tempered chocolate cleanly as it contracts.
The practical test for a distributor: ask the supplier whether their belt is specified for enrobing or cooling tunnel service specifically, or just “food conveying” generally. Esbelt lists cooling tunnel exits as a distinct application with TPU belts capable of withstanding low temperatures while maintaining flexibility for knife-edge configurations . Märtens also lists cooling tunnel service in sweets and chocolate as a named application for their PU belts, citing efficient cold transfer due to low insulation value and good flatness . Those are the suppliers who have thought about this application, not just the material category.
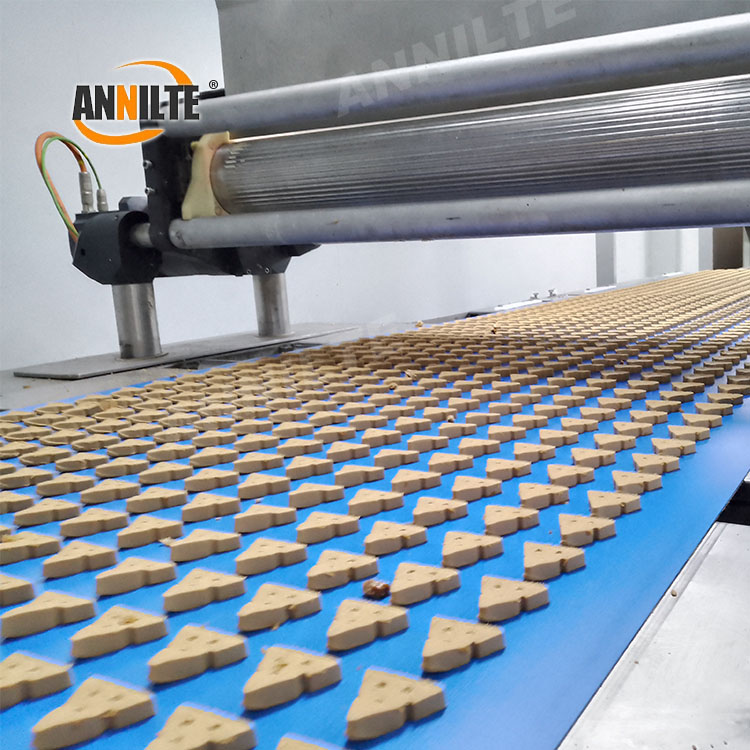
The Residue Problem: Cocoa Butter and Sugar Dust Don’t Clean the Same Way
Chocolate residue in a cooling tunnel is not uniform. You‘re dealing with two different contaminants that behave differently.
Cocoa butter and fat residues liquefy at warm temperatures and solidify as the belt cools. Sugar dust and fine chocolate particles are dry, abrasive, and migrate into splice gaps and edge profiles. A cleaning method that works on one doesn’t necessarily work on the other.
Ammeraal Beltech’s confectionery page is blunt about the operational reality: belts and their components need to be metal-detectable in cocoa processing due to contamination risk, and keeping belts at the required cleanliness level is difficult . That‘s a supplier acknowledging a known pain point rather than glossing over it.
The cleaning technology exists, but it’s worth understanding what you‘re specifying. Steam-based cleaning systems designed for confectionery use high-temperature dry steam (around 120°C surface temperature) with synchronized vacuum extraction. The heat liquefies oils and fats so they can be vacuumed away, while the low moisture content (around 5% water) means the belt is immediately dry and ready to run . A documented case from a German confectionery manufacturer using a steam-and-vacuum system on a line producing chocolate-coated products reported belt cleaning time dropping from 40 minutes to ten, with previously difficult chocolate abrasion removed without residue .
The implication for belt specification: if the customer is using or planning dry steam cleaning, the belt surface needs to tolerate that temperature without degradation. Not every standard PU grade will. This is a question worth asking before the customer buys the cleaning system and then discovers the belt can‘t take the heat.
For buyers not ready for automated steam systems, the belt specification still matters. A smooth, non-porous top surface with minimal splice protrusion reduces the manual scrubbing burden. A rough or textured surface that was chosen for grip will hold onto cocoa butter in exactly the places a brush can’t reach.
The Splice and the Cold: Why Belts Arch and Track Off
Here‘s the problem that rarely makes it into supplier brochures but shows up on every chocolate line eventually.
Ammeraal Beltech lists belt mistracking as a common issue in cooling tunnels, and specifically notes that belt cover imprints can fail to deliver acceptable chocolate embossing, particularly on the splice area of the belt . That’s a polite way of saying the splice behaves differently from the rest of the belt.
A finger splice or toothed splice is a mechanical joint. The material at the joint is either adhesive, fastener, or compressed belt construction—none of which has exactly the same thermal expansion coefficient as the homogeneous belt body. In a cooling tunnel, the belt goes through a temperature cycle on every revolution. Warm side, cold side, warm side again. A splice that was perfectly flat at room temperature can develop a slight lift or wave at tunnel temperature. That lift becomes a catch point, and a catch point becomes a tracking problem.
Märtens lists finger splice, overlapped splicing, adhesive splice, and stainless hook or plastic spiral fasteners as joining methods for their PU belts . For a cooling tunnel, the choice matters more than in ambient conveying. Adhesive splices and finger splices are generally preferred over mechanical fasteners in food cooling applications because they present a more continuous surface and fewer places for chocolate to accumulate. But even a good finger splice needs to be specified for the temperature range the belt will actually see, not the ambient range on the datasheet.
The belt carcass also plays a role in whether the belt stays flat. Märtens emphasizes “excellent lay flat properties” and “good flatness” as PU belt characteristics, and specifically lists cooling tunnel service as an application . That’s not marketing filler—it’s the property that determines whether the belt tracks true through a cold tunnel or starts climbing the side walls after a few weeks.
For a distributor quoting a chocolate cooling tunnel belt, the specification conversation should include: What is the actual tunnel temperature at the belt surface? What pulley diameters are involved at the cold end? Has the splice been tested at that temperature? A supplier who can answer these questions has done this before. One who can‘t is selling you a belt that happens to be food grade, not a belt that’s right for the tunnel.
What to Ask Before You Buy
For plant buyers: Confirm the belt is specified for cooling tunnel service, not just “chocolate conveying.” Ask for the top-surface release characteristic in writing. And if you’re using steam cleaning, confirm the belt’s temperature tolerance at the surface, not just the tunnel ambient.
For distributors: Keep one or two cooling-tunnel-specified PU belts in stock rather than relying on a general food-grade PU that “should work.” The chocolate factories in your territory will pay for the belt that runs without arching, and they‘ll remember who supplied it when the line is down.

R&D Team
Annilte has a research and development team consisting of 35 technicians. With strong technical research and development capabilities, we have provided conveyor belt customization services for 1780 industry segments, and gained recognition and affirmation from 20,000+ customers. With mature R&D and customization experience, we can meet the customization needs of different scenarios in various industries.

Production Strength
Annilte has 16 fully automated production lines imported from Germany in its integrated workshop, and 2 additional emergency backup production lines. The company ensures that the safety stock of all kinds of raw materials is not less than 400,000 square meters, and once the customer submits an emergency order, we will ship the product within 24 hours to respond to the customer's needs efficiently.
As a leading Chinese conveyor belt manufacturer with 17 years of industry experience, Annilte is proud to hold both ISO quality management certification and the RoHS environmental directive. Our manufacturing facilities meet “Green Factory” standards, and we are also an internationally recognized SGS Gold Supplier.
We offer a comprehensive range of customizable belt solutions under our own brand "ANNILTE", designed to meet diverse industrial needs.
Should you require further information about our products or capabilities, please do not hesitate to contact us.
WhatsApp: +86 185 6019 6101 Tel/WeChat: +86 185 6010 2292
E-mail: 391886440@qq.com Website: https://www.annilte.net/
Post time: Nov-16-2026